
A waterjet system does not become safe immediately after the cutting program stops. High-pressure water may remain inside the pump, tubing, valves and cutting head, while the gantry, abrasive delivery system, electrical cabinet and workpiece can retain other forms of hazardous energy.
A safe shutdown procedure must therefore do more than switch off the cutting command. It should stop the cutting cycle in a controlled manner, isolate hazardous energy, release residual pressure, verify that the system has reached a zero-energy state and prevent an unexpected restart before cleaning or maintenance begins.
This guide focuses specifically on shutdown, pressure release, workpiece removal and maintenance preparation. It does not replace the operating manual, lockout/tagout procedure or safety instructions supplied with the installed pump and machine.
A normal waterjet shutdown should follow this general sequence:
Complete or pause the cutting program from the CNC control.
Confirm that the cutting head has stopped moving.
Stop abrasive delivery according to the machine’s control sequence.
Switch off the high-pressure water supply or high-pressure pump.
Operate the manufacturer-approved bleed-down or pressure-release function.
Watch the pressure indication until it returns to the specified safe state.
Isolate electrical, hydraulic, pneumatic and stored-pressure energy when maintenance is required.
Verify that the system cannot restart and that no residual pressure remains.
Remove the workpiece only after cutting motion and high-pressure discharge have stopped.
Clean the work area and record any leakage, abnormal sound or component problem.
The exact sequence can vary with pump design, controller logic, valve arrangement and auxiliary equipment. Operators must follow the instructions supplied with the installed system whenever they differ from this general procedure.
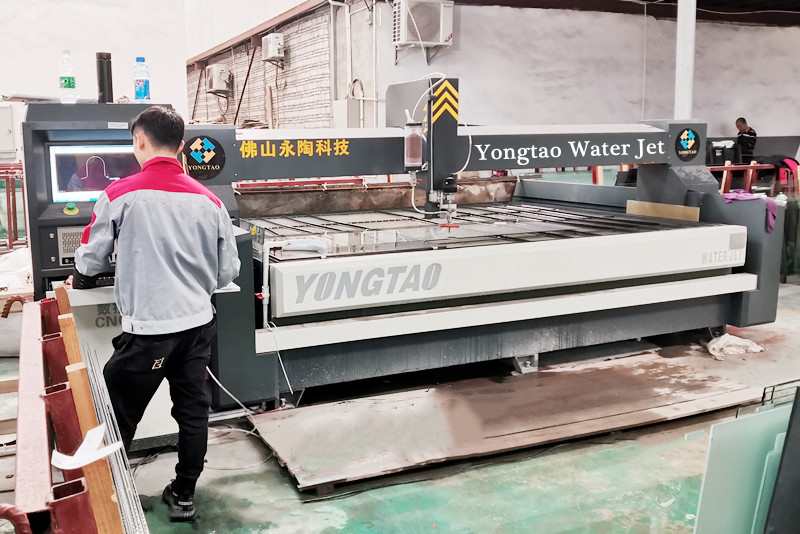
Pressing “stop” on the CNC controller normally ends programmed motion, but it may not isolate every energy source. Depending on the equipment configuration, the pump may remain running, high-pressure water may remain trapped, the abrasive system may still be pressurized, and the axes may still be enabled.
The following hazards can remain after cutting stops:
Residual pressure inside high-pressure tubing and fittings
Pressure retained between check valves or closed valves
Electrical energy in the control cabinet
Hydraulic pressure in an intensifier system
Pneumatic pressure in abrasive delivery equipment
Gravity or stored mechanical energy in moving components
Sharp edges on freshly cut parts and scrap material
Unexpected axis movement caused by an enabled control system
Automatic restart after a temporary power interruption
For this reason, “program stopped,” “pump stopped” and “system safe for maintenance” are three different conditions. Operators should understand the difference before touching the cutting head or opening any high-pressure connection.
A routine production stop may not require the same isolation procedure as maintenance. However, a full lockout/tagout process should be used whenever a person could be exposed to unexpected movement, electrical energy or stored pressure.
Typical tasks requiring complete energy isolation include:
Replacing an orifice, mixing tube or nozzle assembly
Opening high-pressure tubing or fittings
Repairing a leaking connection
Servicing the intensifier or direct-drive pump
Replacing high-pressure seals or check valves
Reaching into a guarded cutting area
Removing jammed material near the cutting head
Repairing the abrasive feed system
Entering the machine envelope
Performing electrical or mechanical maintenance
Turning off a screen, controller or pump button is not necessarily an energy-isolation procedure. The authorized worker should isolate every applicable energy source, apply the facility’s lockout/tagout controls and verify isolation before work begins.
When conditions are normal, allow the cutting program to reach a safe stopping point. If production must be interrupted, use the controller’s pause or controlled-stop function rather than abruptly disconnecting the main power.
A controlled stop helps the system complete the intended cutting-head and valve sequence. It also makes it easier to identify the last completed cutting position if production needs to continue later.
Before proceeding, confirm that:
Programmed cutting motion has stopped
The cutting head is no longer discharging a jet
The axes are stationary
The workpiece has not shifted or lifted
No person is inside the machine operating area
Do not approach the cutting head merely because the visible cutting motion has stopped.
The abrasive supply should be stopped using the sequence specified by the machine manufacturer. Some systems coordinate abrasive delivery automatically with the cutting valve, while others require a separate shutdown command.
Operators should check whether abrasive continues to flow, whether the feed hose is blocked and whether the abrasive vessel remains pressurized. Do not loosen the abrasive vessel cover, hose or connection until its pressure state has been confirmed.
Wet, contaminated or compacted abrasive discovered during shutdown should be recorded for inspection before the next production cycle.
Switch off the high-pressure pump or high-pressure generating function through the normal control interface. On an intensifier system, this may involve stopping the intensifier and hydraulic power according to the manufacturer’s sequence.
The operator should observe the pressure indication and listen for abnormal cycling, leakage or delayed pressure decay. A pump that continues cycling after the cutting head closes may indicate leakage or another problem that requires inspection.
Never assume that stopping the motor immediately removes pressure from the high-pressure circuit.
Use the system’s designated bleed-down valve, dump valve or automatic pressure-release function. The release method must be the one specified for the installed pump and plumbing arrangement.
Do not release pressure by:
Loosening a high-pressure fitting
Partially disconnecting a tube
Removing the nozzle
Opening an unapproved connection
Striking or bending a pressurized component
Using a tool to force a valve into position
High-pressure water may penetrate skin and cause serious internal injury even when the external wound appears small. A suspected high-pressure injection injury requires immediate professional medical evaluation.
Observe the appropriate pressure gauge or controller indication until it reaches the state specified in the operating manual. A zero reading is important, but it should not be the only form of verification when maintenance is planned.
The operator should also confirm that:
The pump cannot restart automatically
The bleed-down cycle has completed
Relevant valves are in their safe positions
No section of tubing is isolated with trapped pressure
Hydraulic or pneumatic accumulators have been addressed
The machine’s energy-isolation procedure has been completed
A faulty, blocked or poorly located pressure gauge may not represent pressure trapped in every section of the circuit. Where the equipment design requires additional verification, follow the manufacturer’s prescribed method.
A verified zero-energy state means hazardous energy has been isolated, released or otherwise controlled so that maintenance can be performed safely.
The verification process should cover all applicable systems.
Confirm that the high-pressure generator is stopped, the approved pressure-release function has operated and the relevant pressure indication has returned to the specified safe state.
Inspect from a safe position for leakage, dripping at unexpected locations or signs that a valve has not closed correctly. Never use a hand or exposed skin to search for a high-pressure leak.
If maintenance exposes a worker to electrical or unexpected motion hazards, isolate the appropriate electrical disconnect. Apply the facility’s lockout/tagout controls and verify the absence of hazardous energy using an approved procedure.
Emergency-stop buttons are safety controls, but they are not normally substitutes for an electrical isolator or formal lockout device.
Intensifier pumps can contain hydraulic energy, while abrasive delivery systems may use compressed air. Both energy sources must be considered before opening covers, vessels, hoses or related components.
Isolate the supply and release stored energy according to the corresponding component manual.
Confirm that the gantry, cutting head, Z-axis and any tilting or rotating axes cannot move unexpectedly. On a five-axis cutting head, stored position and gravity may create hazards that are not present on a conventional three-axis head.
Support or secure components when the maintenance instructions require mechanical restraint.
Nozzle work should begin only after the required energy-isolation and pressure-release steps have been completed.
Before removing any cutting-head component:
Stop programmed motion and high-pressure generation.
Release stored pressure through the approved function.
Isolate the machine against unexpected restart.
Confirm the cutting head is in an accessible, stable position.
Clean loose abrasive and contamination around the assembly.
Use the correct tools specified for the cutting head.
Follow the specified tightening torque and assembly order.
Inspect sealing surfaces and mating parts before reassembly.
Do not grip precision components with unsuitable tools or apply excessive force. Incorrect assembly can damage the orifice, mixing chamber, seals or alignment of the cutting stream.
After replacement, perform the manufacturer’s inspection and test sequence. Keep people away from the cutting area during the first pressurization and check for abnormal leakage from a safe position.
Freshly cut parts can have sharp edges, unstable offcuts and trapped abrasive. Small parts may also fall between the cutting-table slats.
Before removing material:
Confirm that the jet and all axis motion have stopped
Move the cutting head to a designated safe position if required
Isolate the machine when reaching into a hazardous area
Wear suitable eye, foot and cut-resistant hand protection
Use lifting equipment for heavy or awkward workpieces
Check that suspended parts cannot swing into the cutting head
Remove small scraps with suitable tools rather than bare hands
Keep hoses, cables and high-pressure tubing clear of lifting paths
When a crane is used, plan the lifting path before raising the workpiece. The load, hook, sling or lifting beam must not strike the cutting head, abrasive hose, high-pressure tubing, gantry or control equipment.
Do not attempt to reposition a moving or unstable workpiece while the cutting cycle is active.
Cleaning should begin only after the equipment has reached the condition required for the task. Switching off high-pressure water does not automatically make every area safe to enter.
A post-cutting cleaning routine may include:
Removing sharp scrap and loose offcuts
Washing abrasive residue from completed parts
Cleaning standing water from the floor
Checking cutting-table slats for damage
Removing excessive abrasive accumulation
Inspecting drain and filtration areas
Cleaning around the cutting head without disturbing alignment
Returning tools and lifting equipment to designated locations
Do not use hands to sweep sharp fragments. Do not climb or walk on the cutting table unless the machine design and site procedure specifically allow it.
A clean, dry and organized work area reduces slip, trip, handling and restart hazards.
An abnormal condition may require immediate stopping rather than a normal production sequence.
Examples include:
Sudden high-pressure leakage
Hose or tubing movement
Unexpected cutting-head motion
Workpiece displacement
Collision risk
Loss of abrasive flow
Strong vibration or unusual noise
Pressure fluctuation outside the expected range
Guard or interlock failure
Electrical smell, smoke or overheating
Unexpected power failure
Use the emergency-stop function when there is an immediate danger to personnel or equipment. Keep people away from the machine and do not approach a suspected high-pressure leak.
After the immediate hazard has been controlled:
Identify which energy sources may still be present.
Isolate the equipment according to the emergency and lockout procedure.
Release stored pressure only through the approved method.
Prevent an automatic restart.
Inspect the affected components before returning the system to service.
Record the event and corrective action.
The emergency stop should not be reset until the cause has been identified and the restart has been authorized.
A power failure can stop the controller and pump without completing the normal valve or bleed-down sequence. Operators should therefore treat the system as potentially pressurized.
Do not immediately open a high-pressure connection or touch the cutting head. Keep the machine area controlled, isolate the applicable energy sources and follow the manufacturer’s power-failure pressure-release procedure.
Before power is restored, confirm that an automatic restart cannot occur and that personnel, tools and lifting equipment are outside the operating envelope.
The system should not return directly from maintenance to full production.
Before restarting:
Confirm that maintenance work is complete
Check that all tools and temporary supports have been removed
Reinstall guards, covers and safety devices
Confirm high-pressure fittings have been assembled correctly
Check the cutting-head assembly and abrasive connections
Remove lockout/tagout devices through the authorized procedure
Notify affected personnel before re-energizing the equipment
Perform a low-risk inspection or test cycle as specified
Watch for leakage, abnormal noise and unstable pressure
Complete a dry run with the high-pressure jet disabled when appropriate
Conduct a controlled trial cut before resuming production
Do not bypass an interlock or remove a protective cover to accelerate the restart process.
A short shutdown record helps identify recurring problems before they cause extended downtime.
The operator can record:
Date, shift and operator
Final system pressure indication
Whether the pressure-release cycle completed normally
Visible leaks or damaged tubing
Pump cycling or abnormal sound
Nozzle and abrasive-feed condition
Cutting-table and slat condition
Amount of abrasive accumulation
Emergency-stop or interlock events
Maintenance work required before restart
Records are particularly useful when several operators use the same equipment or when pressure instability appears intermittently.
Before leaving the machine or releasing it for maintenance, confirm the following:
Cutting motion has stopped
The cutting jet is off
Abrasive delivery has stopped
The high-pressure source is off
The approved pressure-release sequence is complete
Residual pressure has been checked
Automatic restart has been prevented
Required energy sources have been isolated
Guards and access controls remain effective
Workpieces and scraps have been removed safely
The floor and work area are clean
Abnormal conditions have been recorded
Maintenance personnel have been informed of unresolved problems
This checklist should be adapted to the actual equipment, pump type, control system and factory safety procedure.
A stopped program may leave the pump, axes or auxiliary systems energized. Use the required shutdown and isolation controls for the intended task.
A fitting must never be used as an improvised pressure-release point. Use the designed bleed-down or dump system.
A gauge reading should be considered together with the system design and prescribed verification method. Pressure can remain trapped between closed valves.
Pause is not necessarily a safe-entry state. The machine may resume motion or restart the cutting sequence.
Scrap removal and cleaning can place hands and tools inside hazardous areas. Complete the appropriate isolation steps first.
An emergency stop records a symptom, not its cause. The system should not be reset until the hazard has been assessed.
Safe shutdown is a controlled transition from active cutting to a verified condition in which stored pressure, electrical energy, auxiliary pressure and unexpected movement have been addressed.
The essential principle is simple: stopping the cutting program is not the same as making the equipment safe for contact or maintenance. Operators should use the approved pressure-release function, verify the energy state and follow the machine-specific manual and facility lockout/tagout procedure before opening high-pressure components or entering a hazardous area.
For production facilities comparing equipment layouts after establishing their operating and safety requirements, Yongtao provides information about available 3-axis, AB five-axis and AC five-axis models.
Not necessarily. High-pressure water may remain trapped in tubing, valves or other parts of the circuit. The approved pressure-release or bleed-down sequence must be completed, and the safe state must be verified according to the installed system’s instructions.
No. A fitting should never be loosened as a method of pressure release. Stored high-pressure water can cause serious injury and component damage. Use only the designed pressure-release function.
A zero reading is important, but maintenance may also require electrical, hydraulic, pneumatic and mechanical isolation. The operator should follow the complete machine-specific energy-isolation and verification procedure.
It should be used whenever servicing, cleaning, unjamming or inspection could expose a person to unexpected startup, high pressure, electrical energy, axis movement or another hazardous energy source. Follow the factory’s authorized lockout/tagout program.
Treat the system as potentially pressurized, prevent automatic restart and follow the manufacturer’s power-failure shutdown procedure. Do not open tubing or remove cutting-head components until residual energy has been safely controlled.
No. The emergency stop is intended for hazardous or abnormal situations. A routine shutdown should use the normal controlled sequence unless an immediate danger requires emergency stopping.
Remove the workpiece only after cutting discharge and machine motion have stopped and the equipment has reached the safe condition required for entering or reaching into the work area.
Check all fittings, guards, covers, cutting-head components, tools and safety devices. Remove lockout/tagout controls through the authorized procedure, notify affected personnel and conduct the prescribed inspection and test cycle.
 0086-18665475362
[email protected]
Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China
 0086-18665475362
 [email protected]
 Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China
 English
 Español