
Abrasive waterjet cutting is an erosion-based separation process in which a concentrated stream transfers energy to a workpiece through water and accelerated abrasive particles. Its technical value is not defined by one pressure figure, one accuracy claim or a simple list of materials. It is defined by how the cutting stream interacts with the workpiece from initial entry to final exit.
The principal characteristics of the process include non-thermal material removal, low overall mechanical loading, toolpath flexibility, adjustable cut quality and a predictable difference between the entry and exit sides of the cut. These characteristics affect part design, production planning, edge requirements and the amount of finishing required after separation.
This guide explains these characteristics from an engineering and production perspective. It focuses on what the process does to the finished part rather than on machine selection, operating instructions or individual parameter adjustments.
Abrasive waterjet cutting removes material through high-speed erosion instead of melting it with heat or shearing it with a solid cutting edge. This gives the process six defining characteristics:
Non-thermal material separation
Low overall cutting force
No fixed tool shape controlling the profile
A relatively narrow material-removal path
Selectable cut-quality levels
A gradual change in jet energy through the material thickness
These characteristics allow complex parts to be separated from different material categories while limiting thermal change and heavy mechanical loading. However, the finished result still depends on material thickness, internal structure, part geometry and the quality level required at the exit side.
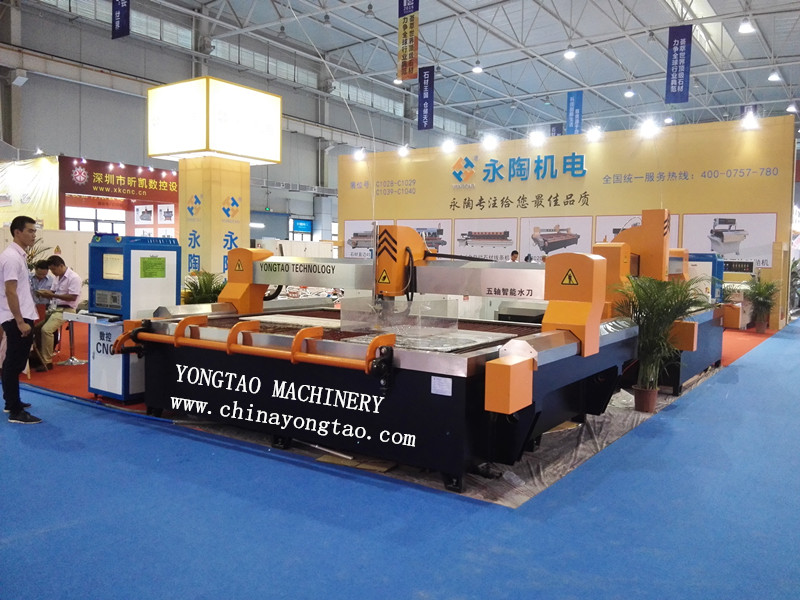
The cutting stream should be understood as a controlled carrier of energy. Water accelerates through a small orifice and transfers momentum to abrasive particles inside the cutting head. The accelerated particles then perform most of the material removal in hard-material applications.
When the stream reaches the workpiece, its energy is highest near the entry surface. As it moves deeper into the material, part of that energy is consumed by erosion, particle breakage, turbulence and interaction with the walls of the developing kerf.
The stream therefore does not behave like a rigid cylindrical tool. It is a flexible, moving erosion stream whose condition changes continuously through the thickness of the workpiece.
This explains several important production characteristics:
The entry edge and exit edge may not be identical.
Thicker materials create a longer energy-transfer path.
Direction changes may affect the lower section of the cut differently from the upper section.
The required edge quality influences allowable production speed.
Material behavior cannot be predicted from hardness alone.
Understanding these relationships is more useful than describing the process only as “high-pressure cutting.”
Abrasive waterjet cutting separates material without relying on a sustained melting or burning zone. Water also removes much of the local energy generated during particle impact.
For production planning, the important result is that the cut edge does not develop the conventional heat-affected condition associated with thermal separation. This can help preserve heat-sensitive surface conditions, coatings, hardness states and material appearance.
The process is therefore valuable when a drawing restricts thermal discoloration, melted edges or heat-related dimensional change. It may also reduce preparation before subsequent welding, bonding or machining.
“Cold cutting” should still be used as a technical classification rather than an absolute claim that no microscopic energy or temperature change occurs. The meaningful production characteristic is the absence of a sustained thermal cutting zone that significantly changes the surrounding material.
A solid cutting tool applies force through teeth, an edge or a contact surface. An abrasive waterjet distributes material removal across many small particle impacts.
This produces relatively low overall cutting force on the workpiece. Heavy clamping is not always required, and the process can be suitable for components that would be difficult to hold against the force of a saw, mill or punch.
Low loading does not eliminate the need for material support. A separated part can move, a narrow section can lose stability, and residual stress inside a plate or slab can be released after cutting. The support arrangement and cutting sequence must therefore reflect the finished part geometry.
The key characteristic is that the cutting process introduces limited bulk force, while the workpiece can still respond to its own weight, internal stress and loss of support.
The cutting profile is determined mainly by CNC movement rather than by the physical shape of a saw blade, drill, punch or forming tool.
One cutting head can follow straight lines, curves, openings and irregular contours without requiring a tool manufactured to match each finished shape. This reduces the need for profile-specific tooling when product designs change frequently.
The process is particularly flexible for:
One-off components
Small production batches
Customized decorative shapes
Parts with several different radii
Nested components with different outlines
Prototype and development work
This does not mean every geometry is equally easy to produce. Very small internal details, narrow bridges, closely spaced piercings and abrupt direction changes must still be evaluated against the stream diameter, material thickness and required exit-side accuracy.
The stream removes a narrow path of material known as the kerf. Because the kerf has measurable width, the programmed path cannot normally be identical to the finished-part boundary.
The CNC program must position the stream on the appropriate side of the drawing line. This relationship affects internal openings, external profiles and the spacing between nested parts.
Kerf should not be treated as one universal dimension. It is a process result influenced by the cutting-head combination, material response and required quality. The important characteristic is that kerf is predictable enough to be considered in programming, but it must be verified for the actual production condition.
A controlled kerf can support efficient nesting because neighboring components may be positioned closer together than with some wider mechanical cutting methods. Sufficient spacing must still be maintained for piercing, part stability and the required quality on both adjacent edges.
Abrasive waterjet cutting does not produce only one standard edge finish. The process can be planned for different levels of separation and surface quality.
A production cut may be selected for:
Fast material separation
General fabrication quality
Reduced lower-edge markings
Improved dimensional consistency
A near-finished visible edge
The most suitable level depends on how the part will be used after cutting. A blank scheduled for machining may only need complete separation and sufficient allowance. A decorative inlay or exposed countertop opening may require a more consistent surface directly from the cutting process.
Higher visual quality generally requires more cutting time. For this reason, specifying the smoothest possible edge for every part can reduce productivity without adding useful value.
Cut quality should be treated as a functional drawing requirement. The selected level should satisfy the next production operation, appearance standard and dimensional tolerance.
The stream enters the material with more available energy than it has near the exit. This entry-to-exit relationship is one of the most distinctive abrasive waterjet characteristics.
The upper portion of the cut generally follows the programmed motion more directly. The lower portion reflects the energy remaining after the stream has travelled through the workpiece.
As material thickness increases, the difference between the upper and lower sections can become more important. This may appear as a difference in kerf geometry, edge texture or the timing of the stream as it follows a change in direction.
The result should not automatically be classified as a machine defect. Some entry-to-exit variation is a normal characteristic of an erosion stream. The production objective is to keep that variation within the tolerance and edge-quality limits required by the part.
Pure-water and abrasive waterjet processes use related technology, but their cutting characteristics are different.
Pure-water cutting uses the concentrated water stream without adding abrasive. It is generally associated with softer materials that can be separated by the water stream itself.
Typical material categories may include:
Foam
Rubber
Textiles
Paper-based products
Some plastics
Soft sealing materials
Pure-water cutting can produce a very narrow cut and avoids embedding abrasive particles in the workpiece. Whether it is suitable depends on material density, thickness, structure and sensitivity to water.
Abrasive cutting adds hard particles to increase erosion capability. It is used when the water stream alone cannot efficiently separate the material.
Typical categories include:
Metals
Natural stone
Engineered stone
Ceramic materials
Non-tempered glass
Composite panels
The abrasive process creates additional considerations, including spent abrasive, catcher-tank accumulation and possible particle contact with the cut surface. These are normal characteristics of the process and should be included in production and waste-management planning.
The distinction between the two methods should be based on material response and the required removal mechanism, not on an assumption that abrasive cutting is always preferable.
Because separation does not depend on melting, the area beside the cut is less likely to experience thermal discoloration, recast material or a heat-hardened edge.
This is relevant when the original material condition must be preserved for later welding, coating, bonding or precision machining.
Low cutting force and limited thermal input can reduce two common sources of dimensional change. However, the finished part can still move when internal material stress is released or when a narrow section loses support.
Dimensional planning must therefore consider both the cutting process and the existing condition of the material.
The edge can range from a basic separation surface to a smoother, more controlled finish. The acceptable condition should be specified before programming begins.
Terms such as “smooth,” “high precision” or “finished edge” are subjective unless they are connected to measurable tolerance, visual samples or the requirements of the next operation.
Some components may move directly to assembly, while others still require machining, polishing, deburring or surface preparation.
The absence of thermal damage does not automatically mean that every edge is ready for final use. Secondary-processing requirements depend on the material, quality level, design and customer acceptance standard.
Different parts can appear similar after nesting and separation. Production planning should therefore include part identification, orientation and removal sequence.
This becomes especially important when several customized shapes, mirrored parts or different quality requirements are processed on the same sheet or slab.
A professional technical description should explain where the process requires additional evaluation.
Tempered glass contains a controlled internal stress pattern. Penetrating its surface usually releases that stress and causes the panel to break. It should not be described as a normal profile-cutting material for abrasive waterjet processing.
Materials that absorb water, react with moisture or contain water-sensitive adhesives require testing. The process may successfully separate the material while still causing swelling, staining, layer separation or later bonding problems.
A laminated material may contain layers with different hardness, density and bonding strength. The stream can interact differently with each layer, so the behavior of the complete structure must be evaluated rather than judging only the outer surface.
Stone, ceramic and non-tempered glass can be processed, but their response to initial penetration must be considered. The risk is affected by internal defects, edge distance, unsupported areas and the design of the starting location.
A drawing may contain an opening, corner or bridge that is smaller than the stable material-removal path. Such features may require a design adjustment, a different starting method or a secondary operation.
The technical ability to cut a material does not automatically make the process the most economical choice. For repetitive thin parts with simple geometry, another separation method may provide a shorter cycle time.
Process selection should consider total production cost, required quality, tooling, material range and downstream operations.
| Characteristic | Production Effect | Important Consideration |
|---|---|---|
| Non-thermal separation | Limits conventional heat-affected conditions around the edge | Some parts may still require secondary finishing |
| Low overall cutting force | Reduces bulk mechanical loading on the workpiece | Parts still require stable support and controlled removal |
| CNC-defined profile | Allows shape changes without profile-specific tooling | Small details must match the physical cutting capability |
| Defined kerf | Supports dimensional compensation and close nesting | Actual kerf must be verified under production conditions |
| Selectable cut quality | Balances productivity with edge requirements | Higher quality normally requires more processing time |
| Entry-to-exit variation | Explains differences through material thickness | Exit-side requirements must be included in inspection |
| Wet erosion process | Captures much of the removed material | Process water, sludge and spent abrasive still require management |
A sample cut should confirm whether the process characteristics match the actual production requirement. The test should use the customer’s real material whenever possible.
Before testing, record:
Material name and grade
Actual thickness
Surface treatment or coating
Required part dimensions
Critical internal and external features
Required edge appearance
Permitted dimensional tolerance
Expected secondary operation
During inspection, evaluate:
Entry-edge condition
Exit-edge condition
Dimensional consistency
Internal-corner appearance
Small-feature stability
Visible surface change
Part movement after separation
Amount of finishing required
A successful sample is not simply one that has been cut through. It is one that meets the dimensional, visual and downstream-processing requirements at an acceptable production rate.
Test results should be stored with the material information and approved drawing. This provides a practical reference for repeat orders and helps prevent subjective quality judgments between different operators.
Technical content should avoid absolute claims such as:
Cuts every material
Produces no waste
Always requires no secondary processing
Creates perfectly vertical edges
Has unlimited thickness capability
Always provides the highest accuracy
More accurate descriptions are:
Suitable for a broad range of materials, subject to material-specific testing
Reduces dry airborne debris while producing process water and settled waste
Can reduce secondary processing when the selected quality meets the final requirement
Can control entry-to-exit variation within application-specific limits
Can process different thicknesses according to material, configuration and quality requirements
Provides controllable accuracy when the full production process is verified
Accurate wording helps engineers, operators and buyers compare process capabilities without confusing general advantages with guaranteed production results.
Abrasive waterjet characteristics are particularly relevant when a project requires:
Limited thermal influence on the material
Different profiles without dedicated shape tooling
Low mechanical force during separation
Processing of several material categories
Controlled nesting of customized components
Defined entry-side and exit-side inspection
Flexible production of prototypes or small batches
An edge suitable for planned downstream processing
The final decision should be based on the complete production requirement. Material name alone is not enough. Thickness, part geometry, tolerance, edge appearance, batch size and subsequent processing determine whether the characteristics of the process provide a practical advantage.
After confirming the material, thickness, part geometry and required edge quality, manufacturers can compare suitable industrial waterjet systems based on table size, axis structure and cutting-head capability.
It is generally classified as a non-thermal erosion process. Material is removed through the high-speed impact of abrasive particles carried by water rather than through melting or a solid mechanical cutting edge.
The most important characteristic is controlled material separation without a conventional heat-affected cutting zone. This allows the process to preserve many of the original properties around the cut edge.
No. The stream is flexible and loses energy while travelling through the material. Its behavior can therefore differ between the entry and exit sides of the cut.
Pure-water cutting relies on the concentrated water stream and is generally used for softer materials. Abrasive cutting adds hard particles so that metals, stone, ceramic and other resistant materials can be eroded more effectively.
No. Low cutting force reduces heavy mechanical loading, but the workpiece still requires appropriate support. Small parts, narrow sections and stressed material can move after separation.
The stream has less available energy near the exit than at the entry. Exit-side inspection can reveal dimensional or surface differences that may not be visible from the top of the workpiece.
No. Edge quality can be selected according to the production requirement. Faster separation and smoother finished edges represent different balances between productivity, cost and surface condition.
Not in every application. It can reduce thermal cleanup and may produce a directly usable edge, but machining, polishing or surface preparation may still be required depending on the drawing and final use.
No. Tempered glass normally fractures when its stressed surface is penetrated. Non-tempered glass may be processed after material condition, support and part geometry have been evaluated.
No. Wet cutting captures much of the removed material, but the process still produces water, spent abrasive and settled material. These outputs must be collected and handled correctly.
Use an actual material sample and inspect entry condition, exit condition, dimensions, small features, surface response and required finishing. A successful test must meet the complete production requirement, not merely cut through the material.
Provide the material name, grade, thickness, sheet or slab size, finished drawing, tolerance, required edge appearance, batch quantity and planned secondary operation. This information allows the test result to be evaluated against a real production target.
 0086-18665475362
[email protected]
Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China
 0086-18665475362
 [email protected]
 Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China
 English
 Español