
Waterjet kerf compensation is the process of moving the programmed toolpath away from the nominal part geometry so that the finished external profile, hole, slot or internal feature remains at the required size after cutting material has been removed.
The CAD drawing normally represents the required finished dimensions. The cutting jet, however, removes a narrow strip of material called the kerf. If the jet centre follows the nominal contour without an offset, an external part will be undersized and an internal opening will be oversized. Correct compensation places the jet centre on the appropriate side of the contour by approximately half of the effective kerf width.
Kerf compensation must be based on an actual cutting test rather than a nominal nozzle dimension alone. Material type, thickness, cutting speed, abrasive delivery, nozzle condition, standoff distance and required edge quality can all change the effective kerf.
For a closed external profile, offset the jet-centre toolpath outward by one-half of the measured kerf width.
For an internal hole or closed internal profile, offset the toolpath inward toward the waste area by one-half of the measured kerf width.
If the measured kerf is 1.00 mm, the initial compensation value is normally 0.50 mm per side. A finished external circle with a required diameter of 100.00 mm therefore uses a jet-centre path of approximately 101.00 mm. A finished internal hole with a required diameter of 100.00 mm uses a jet-centre path of approximately 99.00 mm.
These are starting values. The final offset should be verified by cutting and measuring a test coupon under the same production conditions as the actual part.
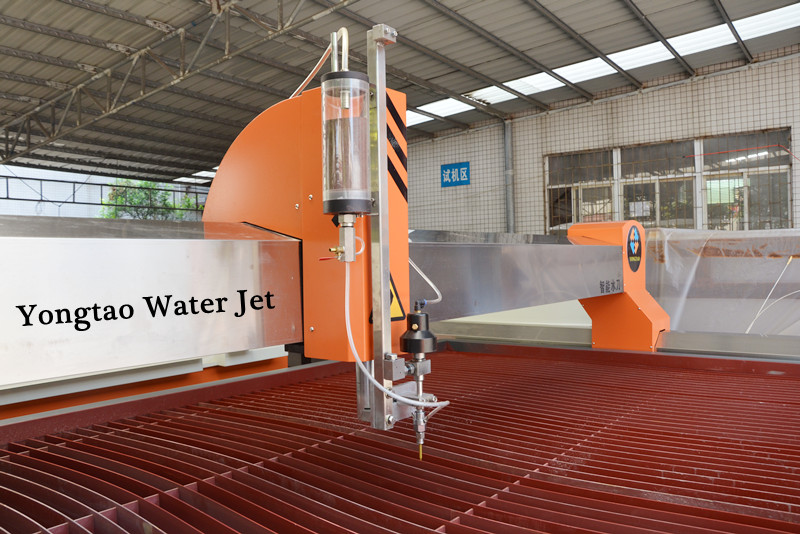
Kerf is the slot created as the abrasive jet passes through the workpiece. It represents the material removed along the cutting path.
Kerf width is related to the cutting stream, but it should not automatically be treated as equal to the mixing-tube diameter. The effective slot can change because the jet loses energy, spreads, deflects and trails as it moves through the material.
The upper and lower parts of the cut may also have different widths. For that reason, a kerf value should always be associated with a defined measurement location, such as:
The top surface of the workpiece
The bottom surface
The middle of the cut edge
A functional inspection plane specified on the drawing
For most routine 2D profile work, the top-surface dimension is used for setup and inspection. Critical parts may require measurements at more than one height to separate dimensional offset from taper error.
Kerf width is the total width of material removed.
Compensation value is normally the radial or one-sided offset applied between the nominal contour and the jet-centre path.
The basic relationship is:
Compensation value = Measured kerf width ÷ 2
If the measured kerf width is 0.90 mm:
Compensation value = 0.90 mm ÷ 2 = 0.45 mm
Entering the full 0.90 mm as a one-sided offset would normally double the intended correction. Always confirm whether the CAM software or CNC controller requests total kerf width, tool diameter, tool radius or a wear-correction value. Different control systems may use different parameter names.
For an external profile, the finished component is inside the cutting path and the surrounding material is waste.
The jet centre must move outside the nominal component boundary. Without this outward offset, part of the required component is removed and the finished profile becomes smaller than the CAD dimension.
For a required 100.00 mm external circle with a 1.00 mm kerf:
Required finished diameter: 100.00 mm
Measured kerf width: 1.00 mm
Radial compensation: 0.50 mm
Approximate jet-centre path diameter: 101.00 mm
The increase in path diameter is 1.00 mm because the centreline is moved outward by 0.50 mm on both sides of the circle.
For an internal contour, the material inside the contour is normally waste and the required component remains outside it.
The jet centre must move inward toward the waste material. If the jet centre follows the nominal hole boundary, it removes material beyond that boundary and produces an oversized opening.
For a required 100.00 mm internal hole with a 1.00 mm kerf:
Required finished hole diameter: 100.00 mm
Measured kerf width: 1.00 mm
Radial compensation: 0.50 mm
Approximate jet-centre path diameter: 99.00 mm
The path diameter is reduced by 1.00 mm because the centreline is moved inward by 0.50 mm around the complete hole.
An open cutting line does not have an automatically defined inside or outside. The programmer must decide which side of the drawing line contains the finished edge.
A slot is more complex because its width is controlled by two opposing cut edges. Before applying an offset, confirm whether the CAD geometry represents:
The slot centreline
One finished edge
Both finished slot boundaries
A single-pass cut
A closed contour used to remove the entire slot
A centreline slot narrower than the effective jet and its required clearance may not be physically achievable. It should not be corrected simply by increasing the compensation value.
An accurate offset begins with a controlled test cut. Do not rely only on a catalogue nozzle dimension or a value used for a different material.
Use the same material grade and approximately the same thickness as the production part. Install the intended orifice, mixing tube and abrasive. Use the same pressure, abrasive flow, cutting quality and traverse-speed settings planned for production.
Secure the coupon in the same way as the actual workpiece. Material movement during piercing or cutting can produce a false dimensional result.
A straight cut is useful for checking the physical slot width. A closed square or circle is more useful for verifying the complete relationship between the CAD geometry, offset direction and finished dimensions.
For precision work, cut both:
An external test coupon
A matching internal opening
This identifies whether a single compensation value produces acceptable results on both types of contour.
Remove loose abrasive, burrs and fragile edge particles without rounding or damaging the measurement surfaces.
Measure with a suitable instrument. A steel ruler is not sufficient for a close-tolerance setup. Depending on the feature, use calibrated callipers, a micrometer, pin gauges, a bore gauge or a coordinate measuring system.
Abrasive waterjet edges can have taper. Measurements taken at the top and bottom may therefore be different.
Measure at the surface or height used for part acceptance. Record that location in the setup sheet so later operators do not compare values taken from different planes.
One cut may be affected by piercing damage, local material variation or measurement error. Cut and measure several features when the tolerance is important.
Use a stable average only after confirming that the results are repeatable. Large variation between identical features indicates a process-stability problem that should be corrected before adjusting the offset.
After entering the initial half-kerf offset, cut a test feature and compare the actual result with the nominal dimension.
For an external dimension:
Correction per side = (Target size − Measured size) ÷ 2
Example:
Target external width: 100.00 mm
Measured external width: 99.80 mm
Total dimensional error: 0.20 mm undersize
Additional outward correction: 0.20 mm ÷ 2 = 0.10 mm per side
For an internal opening:
Correction per side = (Measured size − Target size) ÷ 2
Example:
Target hole diameter: 50.00 mm
Measured hole diameter: 50.16 mm
Total dimensional error: 0.16 mm oversize
Additional inward correction: 0.16 mm ÷ 2 = 0.08 mm per side
The sign and input method depend on the software. Confirm visually that the regenerated toolpath moves farther into the waste area before running the next test.
Kerf compensation may be generated in the CAD/CAM system or applied at the CNC controller. Both methods can be effective, but the same base compensation should not normally be applied twice.
CAM compensation creates an offset toolpath before the program is sent to the machine. This approach is useful because the programmer can inspect the complete path, lead-ins, lead-outs, corners and narrow features before cutting.
The CAM system should clearly identify:
External or male contours
Internal or female contours
Open-path offset direction
Kerf or tool-radius value
Lead-in and lead-out location
Cutting direction
Intersections caused by the offset
After toolpath generation, zoom in on holes, corners and small arcs. Confirm that no feature has disappeared, reversed or created a self-intersecting path.
Controller compensation can allow an operator to make small corrections without regenerating the complete program. It is particularly useful for controlled wear adjustments after the base toolpath has been established.
When the controller supplies the compensation, the CAM-generated base offset must be set according to the machine manufacturer’s workflow. Do not assume that every G-code controller interprets left and right compensation identically.
G41 and G42 selection depends on contour direction, tool movement and which side contains the finished component. The safe procedure is to inspect the displayed path or run a dry simulation rather than selecting a code from memory.
Double compensation occurs when a full kerf offset is created in CAM and another full offset is enabled in the controller.
Possible results include:
Oversized external parts
Undersized internal holes
Distorted small features
Controller alarms
Unexpected path movement at lead-ins
Incorrect fit between mating components
Record where the base compensation is applied. If the CNC control is used only for wear correction, record the permitted adjustment range separately.
A kerf value is a process-specific setting, not a permanent machine constant.
Hardness, density, brittleness, grain structure and thickness affect how the jet transfers energy through the workpiece. Two materials cut with the same nozzle and pressure may not produce the same effective slot or edge condition.
Thicker material also gives the jet more time to spread, lag and lose energy. The difference between the upper and lower kerf can consequently increase.
The orifice forms the high-velocity water stream, while the mixing tube guides the abrasive jet. Wear, damage or misalignment can enlarge or destabilize the stream.
An offset correction may temporarily hide dimensional error caused by a worn component, but it cannot restore a coherent jet. Inspect the consumables when the kerf becomes irregular or changes rapidly.
A fast traverse speed can increase jet lag and lower-edge error. A slower finish-quality pass generally improves edge straightness, but it may also change the effective kerf.
Use the same quality setting for calibration and production. A compensation table created at one speed should not automatically be applied to a substantially different speed.
Stable pressure and consistent abrasive flow help produce a repeatable slot. Pressure fluctuation, abrasive starvation, moisture in the abrasive or an unstable feed rate can cause kerf variation along the contour.
Do not correct an unstable process by repeatedly changing the offset. First restore stable cutting conditions.
Excessive or changing distance between the mixing tube and the material allows the jet to spread before entering the workpiece. A tilted or misaligned cutting head can also produce unequal dimensions on different sides of a feature.
Verify nozzle height, perpendicularity and motion-system alignment before final compensation.
Kerf offset changes the position of the complete toolpath in the XY plane. Its main purpose is to correct the finished feature size at a defined measurement plane.
Taper compensation changes the angle or position of the cutting head to reduce the difference between the upper and lower edge dimensions.
A correct XY offset cannot eliminate a V-shaped cut. Likewise, a five-axis taper-control function does not remove the need to establish the proper contour offset.
If the top of a test part is correct but the bottom is consistently too large or too small, investigate taper, speed, jet lag, nozzle alignment and cutting-head control before changing the basic kerf value.
Offsetting a contour changes its geometry. Small internal arcs and narrow spaces may collapse when the required inward offset is equal to or greater than the available radius.
Before cutting, check whether:
The offset path can pass through every narrow section
Internal corner radii are large enough for the effective jet
Adjacent paths leave sufficient material between them
Small holes have enough room for piercing and lead-in movement
Offset contours intersect or reverse direction
The controller has removed any feature during path calculation
If a feature is too small, increasing or decreasing compensation is not a reliable solution. Consider enlarging the feature, changing the corner radius, using a smaller suitable nozzle setup, moving the pierce point or finishing the feature with another machining process.
Confirm the nominal drawing dimensions and identify all external, internal and open contours.
Select the production material, thickness, nozzle combination, pressure, abrasive rate, speed and cut-quality level.
Inspect the orifice, mixing tube, abrasive delivery, nozzle height and machine alignment.
Cut a representative test coupon using stable production parameters.
Measure the effective kerf and record the inspection plane.
Divide the measured kerf by two to obtain the initial one-sided offset.
Assign external and internal contours correctly in the CAM software.
Generate and visually inspect the offset toolpath, including leads, corners, small arcs and narrow sections.
Confirm that compensation is active in only one primary location unless a documented controller wear adjustment is intended.
Cut an external test feature and an internal test feature.
Measure both features and calculate any fine correction per side.
Repeat the test until the dimensions are stable and within the drawing tolerance.
Save the approved values as a controlled process record for that material, thickness and cutting condition.
A reusable compensation record should contain more than one kerf number. Record:
Material name and grade
Material thickness
Required inspection plane
Orifice size
Mixing-tube size and condition
Working pressure
Abrasive type, mesh and flow rate
Standoff distance
Cutting speed or quality level
Measured upper kerf
Measured lower kerf when relevant
Base compensation value
Controller wear adjustment
External test result
Internal test result
Date and operator
Consumable operating time
This record helps operators reproduce approved cutting conditions and distinguish normal consumable wear from programming errors.
Check whether the external contour was offset outward, whether only half of the total kerf was used as the radial value and whether compensation was actually enabled.
Also inspect for an enlarged or unstable kerf caused by nozzle wear, excessive standoff distance or incorrect cutting parameters.
Check for double compensation, an excessive offset value or an incorrect interpretation of total kerf versus tool radius.
Confirm that the controller has not added another compensation value to a toolpath already offset by the CAM software.
Verify that the hole path was offset toward the internal waste area. Check whether the software classified the contour as an external profile or reversed the intended side.
Look for excessive inward offset, double compensation or a full-kerf value entered where the system expected a radius.
For very small holes, also inspect piercing damage and path distortion.
This pattern may indicate axis calibration, backlash, gantry squareness, nozzle alignment or workpiece movement rather than an incorrect global kerf value.
This is primarily a taper or jet-lag problem. Review cutting speed, thickness, nozzle condition, standoff distance and taper-control settings before changing the XY offset.
For production planning, the selected CNC control, cutting head and software must support a clearly defined contour-compensation workflow.
Kerf is the total slot width removed by the cutting jet. Toolpath offset is the distance between the nominal finished contour and the jet-centre path. The initial one-sided offset is commonly half of the measured kerf width.
The original CAD drawing should normally remain at the required finished dimensions. Kerf compensation is usually applied when the cutting path is created in CAM or by a properly configured CNC compensation function. Manually changing the master drawing can create revision and inspection problems.
If the software requests a radial or one-sided offset, the starting value is normally 0.50 mm. If it requests total kerf or tool diameter, it may require 1.00 mm. Confirm the parameter definition before entering the value.
The cutting jet removes material on both sides of its centreline. If the centreline follows the nominal external boundary, some of the required part is removed. Moving the path outward places the removed material mainly in the surrounding waste.
For a hole, the centre section is waste. Moving the path inward places the kerf inside that waste and protects the required hole boundary. Without compensation, the finished opening becomes larger than its nominal size.
It is not recommended. Changes in material, thickness, nozzle condition, speed, abrasive flow and quality setting can alter the effective kerf and taper. Important jobs should use a verified value for the actual production condition.
They can be combined only under a controlled procedure, such as a fixed CAM base path plus a small documented controller wear correction. Applying full compensation in both locations normally causes dimensional error.
The inward offset may be larger than the available arc radius or narrow feature. This can create a zero-radius, negative-radius or self-intersecting path that the software cannot calculate safely. The geometry or machining method must then be reviewed.
No. Taper compensation controls cutting-head angle to improve edge parallelism. Kerf offset controls the XY position of the toolpath. Precision five-axis cutting may require both functions.
Recalibrate after changing the material, thickness, nozzle combination, quality level or major cutting parameters. Recheck it after consumable replacement, collision, maintenance or any unexplained dimensional change.
Reliable waterjet kerf compensation is not achieved by entering a universal number. It is achieved by stabilizing the cutting process, measuring a representative test cut, applying half of the effective kerf on the correct side of each contour and confirming the result on both external and internal features.
The master CAD geometry should remain at the required finished size. Compensation should be controlled in one clearly documented part of the programming workflow, and dimensional offset should always be distinguished from taper, jet lag, machine alignment and consumable wear.
 0086-18665475362
[email protected]
Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China


YONGTAO Machinery is committed to becoming a trusted global manufacturer of innovative and reliable ceramic, stone, and waterjet cutting machinery. We strive to deliver high-quality equipment and professional solutions that enhance productivity, create lasting value for our customers, and build long-term success with our employees and global partners.
 0086-18665475362
 [email protected]
 Road 3, Wuzhuang Xiaofengtian Ind. Zone, Luocun Town, Nanhai Dist., Foshan, Guangdong, China
 English
 Español